
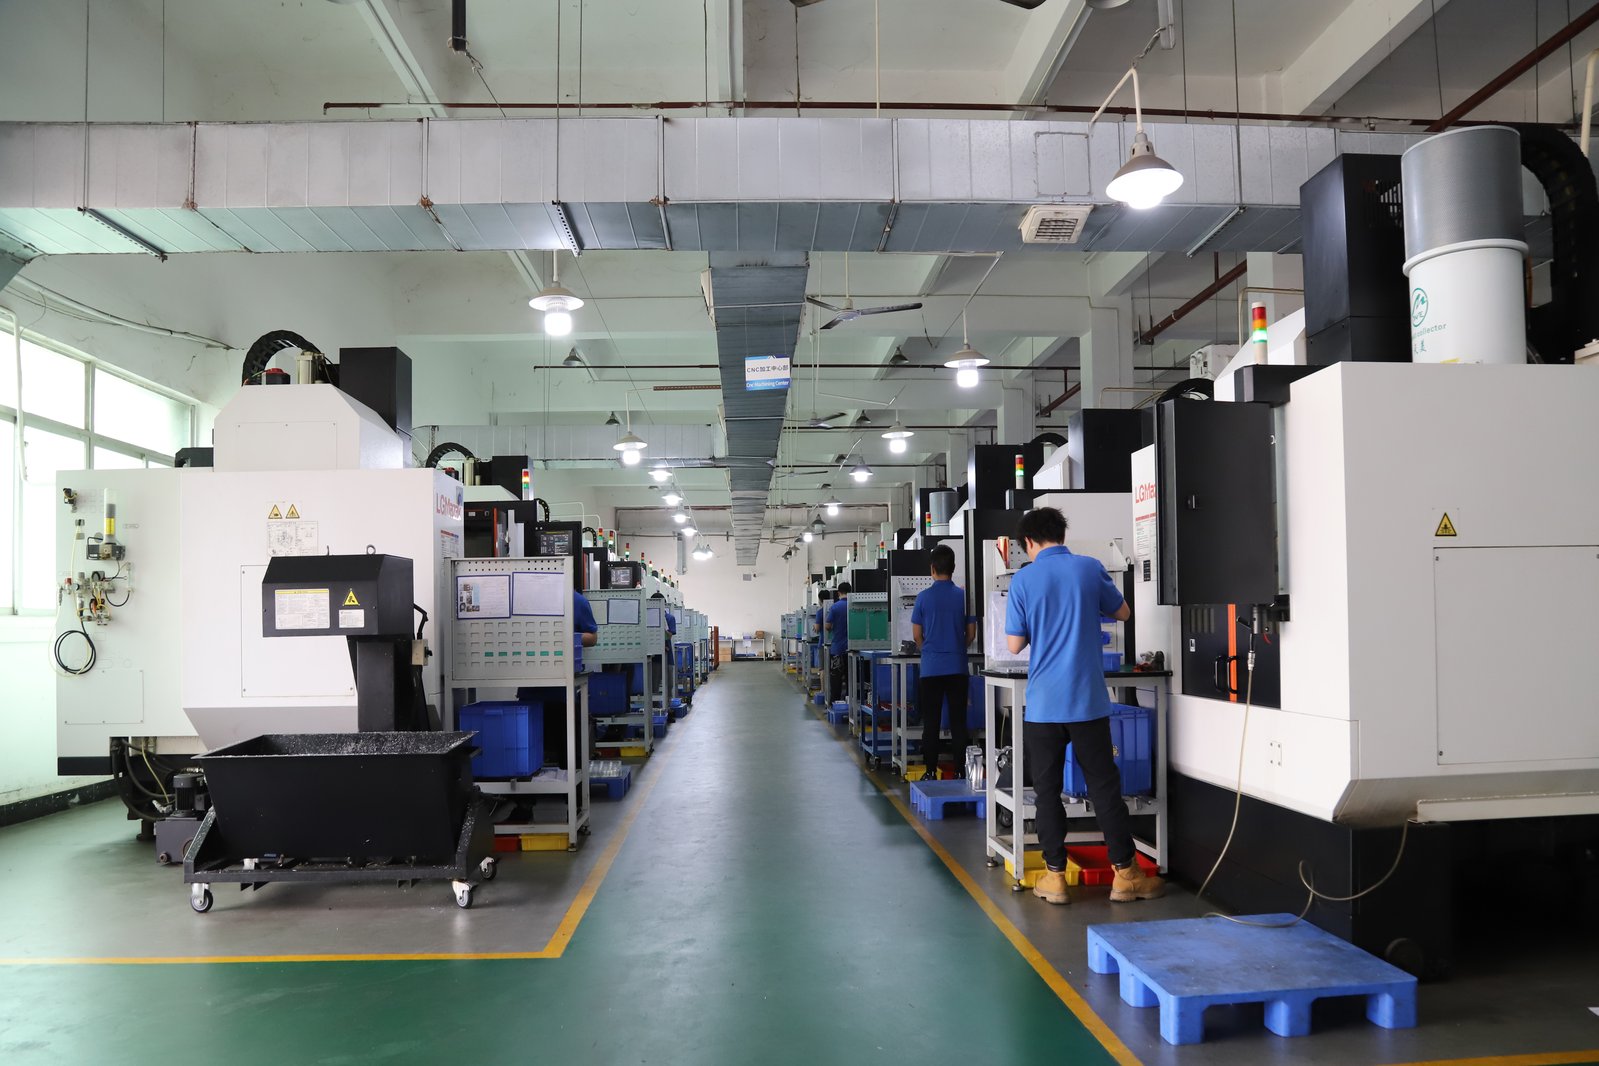
Buyers usually treat a quoted lead time as a statement about machining speed. In practice it is mostly a statement about scheduling, queues, and communication — the cutting time on a typical job is a small fraction of the elapsed calendar. A part can be machined in two hours and delivered in three weeks because it waited in front of a machine, then at a heat treater, then at the measuring room, then for a packing slot and a freight booking.
The useful question is therefore not "how fast can you machine it?" but "where will the days actually go?" Answering that question requires a different kind of estimate: the supplier should be able to name the capacity that will carry your job, the outside operations it will visit, and the approval points that will pause it. This article lays out those levers one by one, and closes with the milestone structure that turns any of them into a date you can manage.
1. Which planning decisions shape a lead time before it is ever quoted?
Lead time does not begin when the purchase order arrives; it begins when the drawing is first reviewed. The completeness of the information package decides how many question rounds the quoting engineer needs, and every round sits on the calendar before the job enters the schedule. A drawing with full dimensions, a named material and condition, and a clear finish callout can move straight to programming, while a sketch with open questions may spend a week bouncing between your engineer and the shop's.
The design-for-manufacturing state matters just as much. A feature that requires an exotic tool, a very deep pocket, or a corner radius at the limit of standard tooling forces special solutions that carry their own procurement and setup time. Catching those issues at the review stage lets the shop order the tooling and plan the setup before your slot arrives, instead of discovering the problem when the job is already in the machine.
Finally, the material decision fixes a supply chain. A stocked grade like 6061-T6 in a standard bar size can be on a machine within a day of approval, while a mill-ordered lot of a specific condition travels for weeks before the first cut. The practical rule is to settle the information, the manufacturability, and the material before the quote is compared, because a date quoted on assumptions cannot be compared with one quoted on decisions.
2. Why does capacity decide your start date more than your part does?
Every shop has a finite number of spindles, and every spindle carries a queue. When your job arrives, it does not simply start; it enters the queue of the machine class that fits its geometry. A shop running near capacity places your order behind existing work, and the width of that queue is usually the largest single component of the elapsed time. This is why two shops can quote very different dates for identical parts: one has an open slot this week, the other is booked for a month.
The distinction that matters is between cycle time and calendar time. Cycle time is the hours the part spends in the machine; calendar time adds the waiting before and between operations. A supplier that quotes a start date, rather than a promise to "begin as soon as possible," is showing you where your job sits in its real load. Ask what machine class your part will run on and how loaded that class is today.
Capacity also explains why small jobs sometimes wait longer than large ones. A high-volume production run can be scheduled predictably around dedicated setups, while a one-off prototype must find spare minutes between committed work. If your schedule is sensitive, ask whether the shop can hold a start date, what happens to that date if another customer's job overruns, and whether expediting is a real option or a phrase that is cheaper to print than to honor.
3. How does quantity change the arithmetic of the calendar?
The quantity on the order changes the schedule's shape, not just its length. A single prototype pays the full cost of programming, tooling, and setup through one part, and its calendar is dominated by preparation rather than by running. A large production quantity spreads the same preparation across thousands of parts, and its calendar is dominated by cycle time multiplied by the batch. The two jobs live in different parts of the planning model.
Between the extremes, the relationship is rarely linear. As quantity grows, the per-part cycle time usually falls — feeds and speeds get optimized, fixtures replace hand setups, and the operator's rhythm improves — until the quantity becomes large enough that the job moves to multiple machines or a second shift, at which point the arithmetic changes again. Ask how the supplier prices and schedules at your specific quantity rather than extrapolating from a per-piece rate.
Quantity also sets the inspection strategy, which is part of the calendar. A prototype gets a full first-article inspection regardless of size. A production batch may be sampled under a defined plan, but a large batch with critical characteristics may still require 100 percent checking of certain features, which adds real hours after the last part is cut. Include the inspection leg in the estimate; it is easy to overlook and expensive to discover.
4. Where do the hidden waiting days sit between operations?
The biggest share of most lead times is spent not in cutting but in waiting. A job moves through a sequence of operations, and between each pair of operations there is a queue: waiting for the next machine, waiting for the heat-treatment batch to fill, waiting for the anodizer's next cycle, waiting for a measuring program. The actual value-added time can be hours while the elapsed time is weeks, and the difference is made entirely of queues.
Outside operations are the most reliable source of hidden days. Heat treatment, plating, anodizing, and specialty grinding are usually done by dedicated suppliers, and each hand-off adds a transport leg and, more importantly, a place at the back of someone else's queue. A part that travels out for hard anodizing and back can gain more calendar than the machining ever consumed. Ask the shop which operations leave the building and how its outside suppliers are scheduled.
The way to see the queues is to ask for the operation list with a date attached to each operation, not one date for the whole job. A supplier that can say "material Tuesday, machining Friday, heat treat the following Monday, return for grinding Wednesday, anodize ships Friday" is showing you the real schedule. A supplier that can only repeat the final date has not looked inside its own calendar, and neither should you.
5. Why does the tolerance map control the inspection leg of the schedule?
Every drawing is inspected, but the inspection effort is set by the tolerance map. A part with a handful of critical characteristics can be verified on a fast sampling plan and released quickly. A part with many features held at ±0.003 mm or finer needs a longer CMM program, more probing time per part, and sometimes 100 percent checking on the critical features, because the risk profile demands it. The machining may be identical; the inspection is not.
The inspection decision also sets the confidence level behind the release. A capability figure such as Ppk ≥ 1.67 initial on a key characteristic only means something if the data behind it is real, which means measurement time was actually spent. When a date is tight, the temptation is to shorten inspection, and that is exactly the wrong corner to cut, because the parts ship either conforming or not, and inspection is the only gate between the two.
Ask about the measurement method at quoting time, not at delivery time. Which features are measured on the CMM, which on gauges, and which are verified at the first article only? What happens to a part whose first article fails — does the clock restart for the whole batch or only for the reworked features? The answers decide whether the inspection leg of your date is realistic and whether a failure costs you a day or a week.
6. How do approvals and documentation pace an overseas order?
An overseas order carries a layer of approvals that a domestic order never sees, and each approval crosses time zones. The drawing confirmation, the first-article review, and the pre-production sign-off all require a question, a wait for the other side's working day, an answer, and usually a second exchange to confirm it. None of these steps involves a machine, yet together they can add more elapsed days than the machining itself.
The pattern is predictable, so it can be managed. Set the approval points when the order is placed and give each one an owner and a deadline on both sides. Agree what happens if a review is overdue — does the production slot get released and re-booked, or does it wait? Decide in advance whether the first-article package is reviewed by your engineer directly or through the supplier's project manager, and keep the review format fixed so no time is lost on interpretation.
Documentation belongs in the same plan. Certificates, dimensional reports, and conformity statements are deliverables with their own preparation time, and a governed industry like aerospace or medical adds format requirements on top. Name the document set in the order, and remember that the clock keeps running while a missing certificate is chased after the parts are ready. Documents finished with the parts ship with the parts; documents chased afterward ship a week later.
7. What happens between a finished part and a delivered part?
The machining calendar ends at the ready date, and a second calendar begins. The part must be cleaned, protected, packaged, and marked against the packing list; the export documents must be assembled; the freight must be booked on a flight or a vessel with space; and the consignment must clear customs at both ends. For a buyer planning a production start, the only date that matters is at the end of this second calendar, not at the end of the first.
The transport method sets the width of that second calendar. Air freight from South China can move a small, urgent consignment in a few days door to door, at a price that scales with weight and volume. Sea freight is dramatically cheaper per kilo and runs in weeks, and it imposes its own rhythm of cut-offs, vessel schedules, and container minimums. The right choice follows the part's weight, its value, and the cost of the days it would lose at sea, and it should be made at quoting so the packaging and documents are planned for it.
The incoterm decides who owns each step. Under DAP the supplier manages the export and the main carriage to your named place; under ex-works everything after the shop's dock is yours to arrange. Neither is better, but the date means something different under each, so state the incoterm next to the date. Ask for the ready date and the delivery date as two separate numbers, and build your schedule from the second one. The range of parts whose freight and handling can be planned this way is shown on the parts page.
8. How do you turn a promised date into a working calendar?
A lead time becomes usable when it is broken into named checkpoints, each with a date and an owner. The practical set runs from drawing approval through material arrival, machining start, first-article review, completion of all operations, the pre-shipment inspection, and the delivery date under the agreed incoterm. A supplier that commits to this list is managing a schedule; one that offers only a final date is managing a hope, and the difference becomes visible the first time something slips.
Milestones need a reporting rhythm to stay alive. Agree that the supplier reports progress at each checkpoint and flags a slip the day it becomes visible, not the day the date passes. The reporting cadence is the early-warning system that lets you move a downstream commitment before it breaks, and it costs nothing to write into the order. Suppliers who run their own scheduling in this shape are easy to recognize, because they volunteer the milestone list before you ask for it. The factory described on the factory page schedules and tracks lots this way.
Finally, tie your payment milestones to the checkpoints you can verify. If the balance of payment releases against the first-article report and the pre-shipment inspection, the supplier's cash flow rewards the schedule that actually happened rather than the one that was promised. Add a modest buffer to the dates you commit to downstream, and you have converted an estimate into a calendar that survives contact with reality.
The buyer's rule of thumb: a lead time is not a machining speed; it is a queueing problem. Find the capacity that will carry the job, the outside shops it will visit, and the approvals it will cross — then write the checkpoints into the order and manage the queue, not the date.
Frequently Asked Questions
What should I ask before comparing China machining lead times?
Ask what the quoted date assumes about the drawing, the material, the quantity, and the inspection level, and ask how much of the calendar is occupied by machine capacity rather than by work content. Two suppliers can quote the same geometry and give different dates simply because one has an open slot and the other does not, so the date is only comparable when the assumptions match.
Why does the schedule sometimes wait on the supplier's other customers?
Machine capacity is shared across all the jobs on the floor. A shop at full utilization will place your order behind existing work, while a shop with an open spindle can start yours sooner. Ask whether the quote reflects an available slot, what load the relevant machine class is carrying, and whether a confirmed start date can be written into the order.
How do order quantities change the arithmetic of a schedule?
Setup and programming time is spread over the quantity, so a one-off pays all the preparation while a large run spreads it thin. Between those extremes the per-part cycle time usually falls with quantity up to the point where multiple machines or shifts are added. Ask how the supplier counts setup, how cycle time scales, and when a batch triggers a different scheduling method.
Where do the hidden waiting days hide in a machining schedule?
Between operations rather than inside them. Parts wait in queues: in front of the heat treater, the anodizer, the plating line, and the measuring room. A job can have very little actual cutting time and still take weeks because it visits four outside shops and waits at each one. Ask which operations leave the building and how long the outside queue usually runs.
How does the tolerance map influence the delivery date?
Tight features decide how the part is measured, and measurement time is part of the calendar. A drawing with many critical characteristics at ±0.003 mm or finer needs a longer inspection program and sometimes 100 percent checking, while a drawing with a few controlled features can be released on a faster sampling plan. The tolerance map should be read together with the inspection method before a date is trusted.
What approval steps slow down an overseas machining order?
Drawing confirmation, first-article review, and pre-production sign-off all cross time zones and inboxes. Every round trip adds at least a day of latency, and a review that needs three exchanges can add a week of elapsed time without any machining happening. Agree the approval points in advance and assign an owner and a deadline to each one.
What happens between finished parts and parts in your hand?
A separate chain runs after the machining date: packaging, export documentation, the freight booking, the crossing itself, and customs at both ends. Air moves small consignments in days while sea moves large ones in weeks, and the incoterm decides which side owns each step. Ask for the ready date and the delivery date as two numbers, and plan from the second one.
How do I turn a promised lead time into a working calendar?
Write named milestones into the purchase order, assign a date to each, and require a progress report against them at a fixed rhythm. Build a small buffer into the dates you commit to downstream, and make payment milestones follow verifiable events such as the first-article report and the pre-shipment check. A date with named checkpoints behind it is a plan; a single round number is a wish.
Need a China machining schedule you can build on?
Send the drawing and your target date through the contact page — the review comes back with the capacity plan, the outside-operation list, and the milestones laid out from approval to delivery.